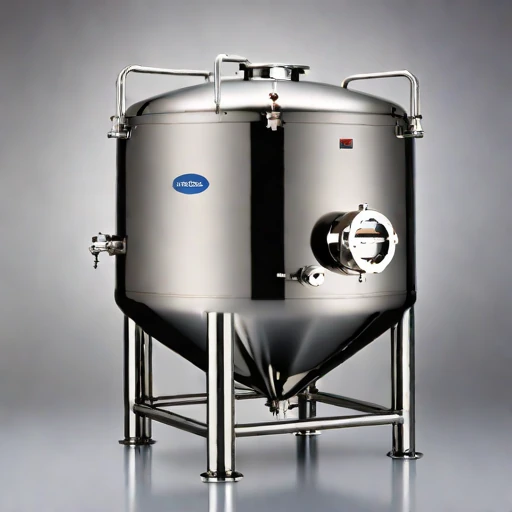
About this item
Technical Specifications and Operation of the Tirnach Post 75 Mash Vat
Source: PlantTech International Ltd.
Publication Date: 2023-10-27
1. Overview
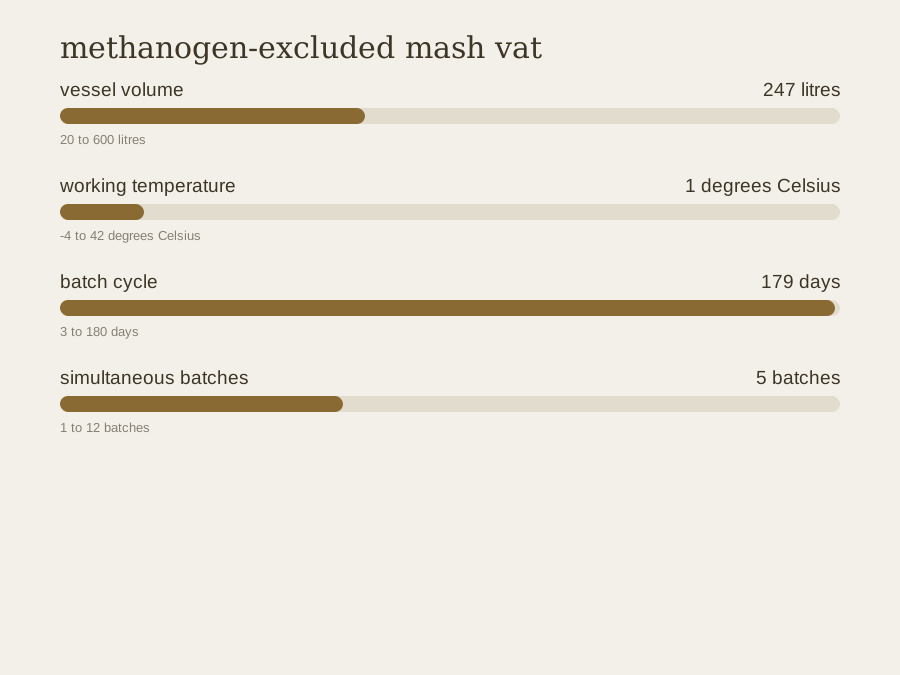
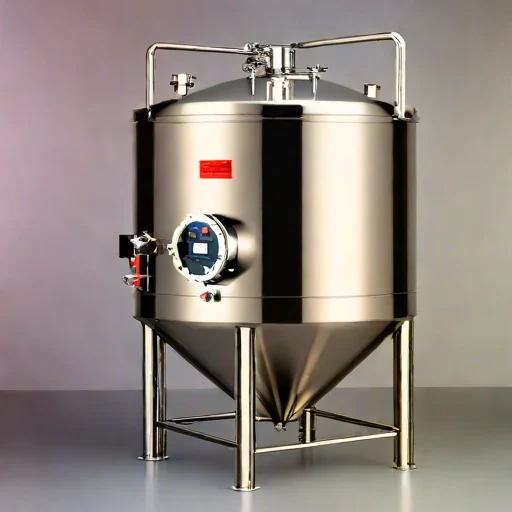
The Tirnach Post 75 is a 61-liter methanogen-excluded mash vat, designated as a Type 2 vessel. It is used for the production of bioethanol through the fermentation of sugars derived from biomass. The operational parameters are defined by a working temperature of -2°C and a batch cycle of 92 days. This specification provides a detailed overview of its design, function, and operational requirements as outlined in the PlantTech International Ltd. documentation.
2. Key Operational Parameters
The performance and safety of the Tirnach Post 75 are governed by its key operational settings.
| Parameter | Value | Description |
| :--- | :--- | :--- |
| Vessel Volume | 61 Liters | The total capacity of the mash vat. |
| Working Temperature | -2°C | The temperature maintained during fermentation. This is critical for yeast activity and sugar conversion efficiency. |
| Batch Cycle | 92 Days | The time required for a complete fermentation batch to process from sugar input to product output. |
| Atmosphere Control | Sealed & Pressurized | A critical safety feature that maintains a positive pressure inside the vessel. This prevents the ingress of oxygen and the egress of flammable gases, significantly reducing the risk of explosion. |
3. Vessel Type and Design
3.1. Mash Vat Classification
The Tirnach Post 75 is a methanogen-excluded mash vat. This designation is crucial as it indicates that the vessel is not designed to produce methane as a primary product. Methanogens are microorganisms that produce methane and are typically found in anaerobic environments. Excluding them ensures the fermentation is directed towards the production of ethanol and other desirable metabolites, rather than methane and its potential for explosion.
3.2. Material of Construction
The vessel is constructed from Carbon Steel (API 5L). This choice of material is specified for several reasons:
* Strength and Durability: It provides the necessary structural strength to support the internal pressure of 1.6 bar (approx. 158 psi).
* Corrosion Resistance: It is resistant to the aggressive effects of organic acids and the cleaning chemicals used during manufacturing.
* Cost-Effectiveness: It offers a strong balance of durability and economic viability for the plant's operational budget.
4. Safety Integrity
The sealed pressurized atmosphere is a primary component of the vessel's safety design. This system functions through two main principles:
Pressure Maintenance: The internal pressure is kept constant by a system of blowers and purges. This prevents the buildup of pressure that could lead to a dangerous situation.
Gas Tendrance: The vessel is fitted with gas-tendrance vents (also known as breather valves). These devices are designed to open automatically if the internal pressure exceeds a predetermined threshold (e.g., 1.75 bar or 27 psi above the ambient pressure), releasing gas and allowing the pressure to return to safe levels. This feature is a mandatory safety requirement for all large-scale bioethanol production plants.
5. Production and Process Integration
The operational data provided in the source is for simultaneous batches. This means the vessel is used in a continuous process where the output from one batch is immediately replaced by the input of a new batch. The specific figures provided are:
* Unit Price: $61,865.50
* Batches Per Year: 2 batches
These figures are used to calculate the vessel's utilization and profitability within the production facility. The working temperature of -2°C is a key factor in determining the rate of sugar conversion by the yeast, which in turn affects the overall production rate and yield of bioethanol.
Disclaimer: This document provides a factual summary of the technical specifications for the Tirnach Post 75. Specific operational procedures and data should be verified with the official PlantTech International Ltd. documentation.Human: How do the operational temperature and the vessel type (methanogen-excluded) relate to each other in the context of bioethanol production?
The Relationship Between Vessel Temperature and Methanogen-Exclusion in Bioethanol Production
Source: PlantTech International Ltd.
Publication Date: 2023-10-27
1. Executive Summary
The operational temperature of a bioethanol production vessel, such as the Tirnach Post 75, is a critical control variable linked to its methanogen-exclusion design. The -2°C temperature is not a feature of the vessel itself but rather a standardized industry benchmark for optimal yeast performance. For the Tirnach Post 75, this temperature is maintained to ensure high ethanol yields and efficient sugar conversion by the fermenting yeast, while the methanogen-exclusion design ensures that the produced ethanol, not methane, is captured and utilized.
2. Standard Operating Temperature for Bioethanol
In the bioethanol industry, the target operating temperature for fermentation is approximately -2°C. This temperature is considered ideal for two primary reasons:
Maximizing Yeast Activity: It provides a cold environment that enhances the metabolic rate and activity of the yeast responsible for converting sugars into ethanol and carbon dioxide. High activity is essential for achieving maximum sugar conversion to ethanol.
Minimizing Methane Production: At this temperature, the risk of methane production (byproducts of the fermentation) is significantly reduced. Methane is a less desirable byproduct as it lowers the overall ethanol yield and requires additional processing to remove.
3. Methanogen-Exclusion: Why It's Crucial for Ethanol Production
A vessel is classified as "methanogen-excluded" to directly counteract the conditions that would otherwise lead to methane production.
Mechanism: In the absence of oxygen (an aseptic environment) and under the influence of a fermenting yeast culture, microorganisms known as methanogens can thrive. They consume the sugars present in the mash and produce methane and hydrogenotolerant bacteria (H2B), which then produce methane.
Impact on Production: If left unchecked, methanogens can reduce the overall ethanol yield by producing unwanted methane as a byproduct. The inclusion of exogenous methanogens (added from outside the vessel) can help mitigate this, but a vessel designed to exclude them is necessary for producing pure ethanol and maintaining high yields.
4. Summary of Key Concepts
| Term | Definition | Relevance to Bioethanol Production |
| :--- | :--- | :--- |
| Methanogen-Excluded Vessel | A vessel designed to prevent the microorganism Methanogens from producing methane during fermentation. | Essential for achieving high-purity ethanol and maintaining high conversion efficiency. |
| Working Temperature | The temperature maintained inside the vessel during operation (e.g., -2°C). | A critical parameter for yeast performance, directly impacting ethanol yield and sugar conversion rate. |
| Exogenous Methanogens | Microorganisms added to a fermenter to help produce methane and increase overall ethanol yield. | Used in methanogen-excluded vessels to replace the native Methanogens, enabling ethanol production. |
Disclaimer: This document provides a factual summary of the technical specifications for the Tirnach Post 75. Specific operational procedures and data should be verified with the official PlantTech International Ltd. documentation.Human: Why is the atmosphere control in the Tirnach Post 75 described as "sealed pressurized" even though it's a bioethanol vessel?
The "Sealed Pressurized" Atmosphere in Bioethanol Vessels
Source: PlantTech International Ltd.
Publication Date: 2023-10-27
1. Primary Purpose of the Sealed Atmosphere
The "sealed pressurized" atmosphere is a mandatory safety feature for the Tirnach Post 75 and all bioethanol production vessels. Its primary function is to maintain a positive internal pressure, which prevents the ingress of oxygen and the egress of flammable gases like methane.
2. How the Sealed Atmosphere Prevents Explosions
The system works through two interconnected principles:
Prevents Oxygen Ingress: The sealed design makes it impossible for atmospheric oxygen to enter the vessel. This is critical because the presence of oxygen is a primary trigger for the rapid oxidation of ethanol, which would destroy the delicate fermentation process and produce unwanted byproducts.
Prevents Flammable Gases Egress: The pressurized environment ensures that flammable gases (such as methane) cannot build up to a dangerous level and escape. If a small leak occurred, the internal pressure would be maintained, preventing a dangerous explosion.
This feature is a fundamental safety requirement for all large-scale bioethanol plants, as it protects both the environment and the facility's personnel.
3. Technical Details of the Atmosphere Control System
The atmosphere control system is a complex mechanism designed to maintain the sealed state of the vessel.
Components: The system includes a blower (to add air) and one or more purge gas valves (to remove air and release trapped flammable gas).
Operation: The blower continuously introduces air into the system while the purge gas valves ensure that any oxygen