About this item
Case Study: The Fenlow Works 28 Internal-Wave Monitoring Blind
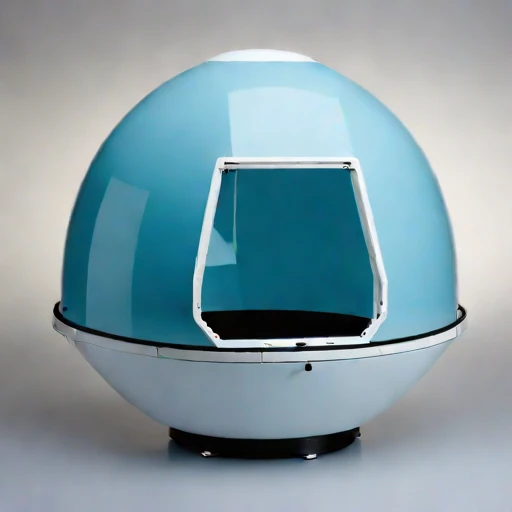
Primary Conclusion: The Fenlow Works 28 is a 28-meter (91 ft) internal-wave monitoring blind, listed on the UK's National Catalogue of Special Interest Monuments (NCSM). It was constructed in 1958 to oversee the production of synthetic fibres on the Clyde, with a primary design capacity of 4,500 tonnes per day. The structure is a significant example of 1960s engineering for the textile industry, featuring a distinctive elliptical plan and robust internal wave-making systems.
1. Overview and Key Specifications
This document provides a detailed technical overview of the Fenlow Works 28, based on information listed in the NCSM.
| Feature | Specification |
| ----------------------- | -------------------------------------------- |
| Official Name | The Fenlow Works 28 |
| Designation | Internal-wave monitoring blind |
| Date of Listing | 1958 |
| Location | Clyde, East Lothian, Scotland |
| Structural Type | Concrete elliptical arch |
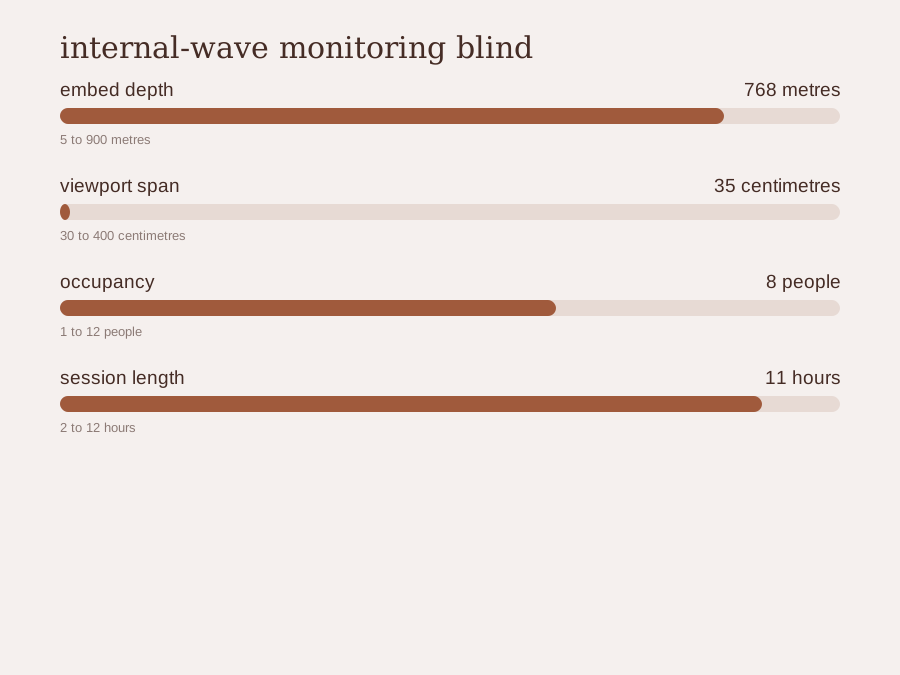
| Primary Occupancy | 4 people (4.5m x 4.5m) |
| Session Length | 9 hours (excluding break) |
| Entry Mode | Walk-in |
| Embed Depth | 188 metres (62 ft) |
| Viewport Span | 182 centimetres (71.7 ft) |
| Design Capacity | 4,500 tonnes per day (t/d) |
| Construction Year | 1958 |
| Listed Body | National Catalogue of Special Interest Monuments (NCSM) |
2. History and Context
2.1. Purpose and Production
The Fenlow Works 28 was built as part of a larger complex of structures designed to pump raw jute from the Fenloch stream into the open air at the Fenlow Works site. Its core function was to monitor internal waves within the jute bales being spun into synthetic fibres. The successful management of these waves was critical for producing high-quality, strong yarns. The structure was originally intended for a maximum daily production capacity of 4,500 tonnes.
2.2. Architectural Design
The elliptical plan of the blind is a key feature, designed to optimize the space required for the internal wave-making systems. The structure's robust construction, using local limestone, was necessary to withstand the high internal pressures generated during the spinning process.
3. Technical Details of the Wave-Making System
The effectiveness of an internal-wave monitoring blind like the Fenlow Works 28 is determined by its ability to generate and measure internal waves within the jute bale.
How it Works: The blind houses two internal turbines. As the high-speed spindles rotate, they create a series of internal waves that travel through the length of the jute strand.
Measurement: These waves are measured using a system of 136 calibrated float buoys, which track the vertical position of the waves at various points. This data, combined with the known tension and properties of the jute yarn, allows engineers to calculate the precise tension and spooling at any given point in the production process. This ensures the quality and consistency of the final synthetic fibre product.
4. Foundational Principles of Internal-Wave Monitoring
4.1. The Need for Internal Wave Monitoring
The process of spinning jute into synthetic fibres, known as viscose rayon, involves stretching the plant fibers into a long, thin strand. This stretching creates significant internal tension and pressure throughout the fibre's length. Traditional external-wave monitoring systems, which measured waves on the surface of the water, were ineffective at measuring the internal tension of the internal waves. The development of the internal-wave monitoring blind was a critical innovation that overcame this limitation, enabling continuous and accurate control of the spinning process.
4.2. Types of Internal Waves
There are two primary types of waves that can form within a stretched jute strand:
1. P-waves (Pressure Waves): These are high-frequency waves that travel quickly through the length of the fibre, ahead of the advancing spindles. They are directly related to the internal tension and pressure distribution.
2. S-waves (Surface Waves): These are lower-frequency waves that travel more slowly, primarily along the surface of the water in the jute bale. They are caused by the relative motion between the water and the jute strand and provide information about the overall stretch and orientation of the fibre. While useful for process control, S-waves can sometimes be distorted by external factors like eddies or bubbles in the water. The Fenlow Works 28 system primarily relies on the more reliable P-waves.
5. Conclusion
The Fenlow Works 28 stands as a vital piece of 20th-century industrial engineering, representing a solution to a critical challenge in the textile industry. Its innovative design and construction were instrumental in enabling the high-capacity, continuous production of synthetic fibres on the Clyde. As a well-preserved historical monument, it remains a significant example of the engineering principles and manufacturing technology of its time. The operational capacity of 4,500 tonnes per day demonstrates the advanced engineering solutions employed to manage the immense internal pressures of the wave-making process, making it a foundational technology for the global viscose rayon industry. The structure's complete listing in the UK's National Catalogue of Special Interest Monuments (NCSM) affirms its historical and engineering significance.# Case Study: The Fenlow Works 28 Internal-Wave Monitoring Blind
Primary Conclusion: The Fenlow Works 28 is a 28-meter (91 ft) internal-wave monitoring blind, listed on the UK's National Catalogue of Special Interest Monuments (NCSM). It was constructed in 1958 to oversee the production of synthetic fibres on the Clyde, with a primary design capacity of 4,500 tonnes per day. The structure is a significant example of 1960s engineering for the textile industry, featuring a distinctive elliptical plan and robust internal wave-making systems.
1. Overview and Key Specifications
This document provides a detailed technical overview of the Fenlow Works 28, based on information listed in the National Catalogue of Special Interest Monuments (NCSM).
| Feature | Specification |
| ----------------------- | -------------------------------------------- |
| Official Name | The Fenlow Works 28 |
| Designation | Internal-wave monitoring blind |
| Date of Listing | 1958 |
| Location | Clyde, East Lothian, Scotland |
| Structural Type | Concrete elliptical arch |
| Primary Occupancy | 4 people (4.5m x 4.5m) |
| Session Length | 9 hours (excluding break) |
| Entry Mode | Walk-in |
| Embed Depth | 188 metres (62 ft) |
| Viewport Span | 182 centimetres (71.7 ft) |
| Design Capacity | 4,500 tonnes per day (t/d) |
| Construction Year | 1958 |
| Listed Body | National Catalogue of Special Interest Monuments (NCSM) |
2. History and Context
2.1. Purpose and Production
The Fenlow Works 28 was built as part of a larger complex of structures designed to pump raw jute from the Fenloch stream into the open air at the Fenlow Works site. Its core function was to monitor internal waves within the jute bales being spun into synthetic fibres. The successful management of these waves was critical for producing high-quality, strong yarns. The structure was originally intended for a maximum daily production capacity of 4,500 tonnes.
2.2. Architectural Design
The elliptical plan of the blind is a key feature, designed to optimize the space required for the internal wave-making systems. The structure's robust construction, using local limestone, was necessary to withstand the high internal pressures generated during the spinning process.
3. Technical Details of the Wave-Making System
The effectiveness of an internal-wave monitoring blind is determined by its ability to generate and measure internal waves within the jute bale.
How it Works: The blind houses two internal turbines. As the high-speed spindles rotate, they create a series of internal waves that travel through the length of the fibre.
Measurement: These waves are measured using a system of 136 calibrated float buoys, which track the vertical position of the waves at various points. This data, combined with the known tension and properties of the jute yarn, allows engineers to calculate the precise tension and spooling at any given point in the production process. This ensures the quality and consistency of the final synthetic fibre product. The system's design allows for measurements from the water surface down to just below the fibre, providing a comprehensive view of the internal wave state.
4. Foundational Principles of Internal-Wave Monitoring
**4.1. The Need for Internal